
 +86 13600513715


News


0102030405
Comparative Analysis of MBBR vs. AAO Wastewater Treatment Processes: Performance, Energy Efficiency, and Optimization Strategies
2026-01-16
Analysis of Operation Performance and Energy Efficiency Assessment for MBBR and AAO Processes
Overview
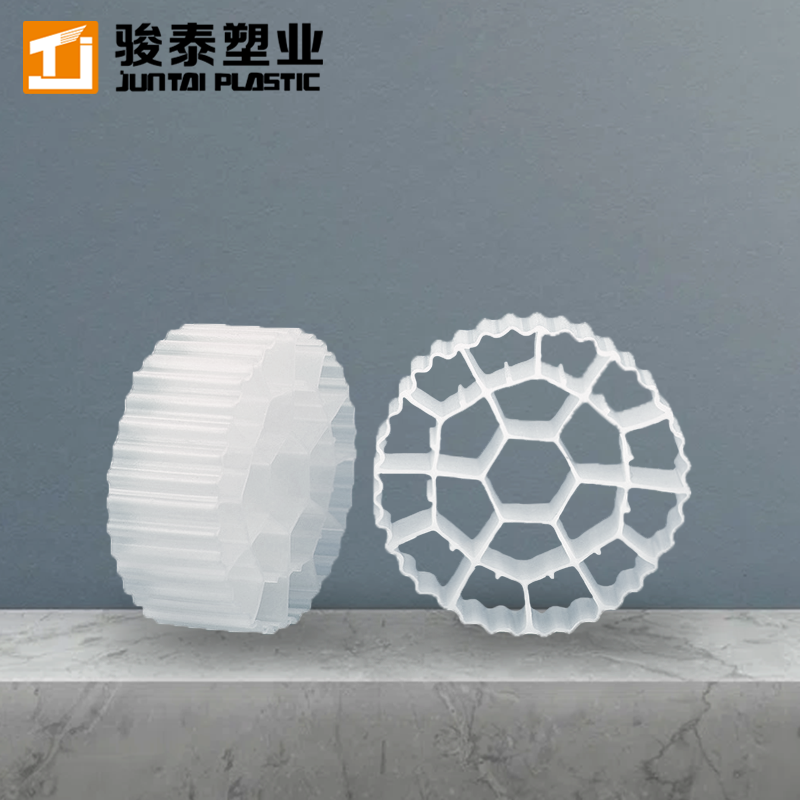
With the comprehensive advancement of the Beautiful China Initiative, China has entered a stage of high-quality development characterized by greening and low-carbon transition. Various regions have successively introduced stricter wastewater discharge standards. Against this backdrop, the Moving Bed Biofilm Reactor (MBBR) is a novel process that has gained significant attention in domestic and international wastewater treatment plants in recent years. It was initially developed by a Norwegian company in the late 1980s. The process involves adding suspended carriers with a density lower than water to the biological reaction tank to increase the biomass in the system, creating a three-phase biological growth environment of gas, liquid, and solid. This significantly enhances the system's treatment capacity without the need for additional land, tank volume, or structures, meeting increasingly stringent effluent quality requirements.
To tap into the treatment potential of existing process structures and accelerate renovation cycles, many traditional Anaerobic-Anoxic-Oxic (AAO) process wastewater treatment plants have been upgraded by adding suspended carriers to their original tanks, transforming them into hybrid biofilm-activated sludge Mbbr Processes. This type of upgrade has been widely promoted in China, with an application scale exceeding 8 million cubic meters per day. Wu Di et al. analyzed the effects of an MBBR process upgrade in a wastewater treatment plant in Shanxi, confirming the enhancement of denitrification capacity and treatment stability due to the carriers. Sun Xiao et al. studied the impact of adding suspended carriers on the original AAO system, showing that the carriers effectively enriched nitrifying functional bacteria, leading to a significant improvement in nitrification capacity. However, there is still a lack of comprehensive research on the energy efficiency of the process after such upgrades and the optimization effects of proposed energy-saving measures based on such assessments.
To comprehensively evaluate the differences in comprehensive energy efficiency between MBBR and AAO processes, this study takes a wastewater treatment plant in Shanghai that operates both MBBR and AAO process lines as an example. It analyzes the operational performance and energy consumption levels of the two processes and proposes related energy-saving optimization measures. The research findings can provide references for process selection and energy efficiency optimization in wastewater treatment plants.
1 Materials and Methods
1.1 Overview of the Wastewater Treatment Plant
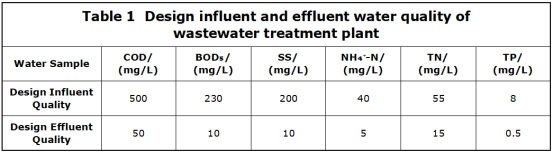
The wastewater treatment plant is located in a chemical industrial park in Shanghai, serving a population of approximately 1 million. The total design capacity is 200,000 cubic meters per day. The first-phase project uses the MBBR process with a design flow of 100,000 m³/d; the second and third-phase projects use the AAO process, each with a design flow of 50,000 m³/d. The influent sources include domestic sewage and industrial wastewater, with industrial wastewater accounting for a relatively high proportion, resulting in high concentrations of various pollutants. The effluent quality meets the Grade A standard of the "Discharge Standard of Pollutants for Municipal Wastewater Treatment Plants" (GB 18918-2002). The design influent and effluent quality are shown in Table 1.
Domestic sewage and industrial wastewater meeting the acceptance standards are collected and transported via the sewer system to the influent pump station, then sent to the coarse screens, fine screens, and vortex grit chambers of the MBBR and AAO processes, respectively. Afterward, they are pumped into the integrated tank. Following treatment in the integrated tank, the flow enters the biological reaction tank (the first three compartments of the MBBR process biological reaction tank have suspended carriers added with a filling ratio of 57%). The effluent from the biological reaction tank enters the flocculation reaction tank and the horizontal-flow secondary sedimentation tank. The secondary sedimentation tank effluent then enters the effluent pump station for chlorination disinfection before discharge. The wastewater treatment process flow is shown in Figure 1.
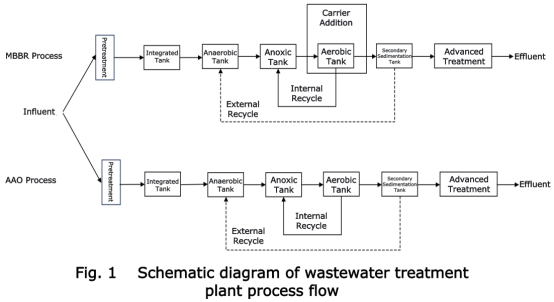
The MBBR process has two biological reaction tanks, each with a treatment capacity of 50,000 m³/d. For each tank, the effective volumes of the anaerobic zone, anoxic zone, and aerobic zone are 2,784 m³, 11,078 m³, and 11,136 m³, respectively. The first compartment of the aerobic zone is designated as the anoxic zone, i.e., the facultative zone. The effective water depth is 5.8 m, the external sludge recirculation ratio is 100%, the internal recirculation ratio is 300%, and the design Hydraulic Retention Time (HRT) is 17.3 hours. Specifically, the anaerobic zone HRT is 1.3 h, the actual anoxic zone HRT is 5.3 h, with 1,400 m³ of carriers added to achieve a design HRT of 6.5 h; the actual aerobic zone HRT is 5.4 h, with 4,800 m³ of carriers added to achieve a total design HRT of 9.5 h. The Mixed Liquor Suspended Solids (MLSS) concentration in the aerobic tank is maintained at 3.0 g/L. The design air-to-water ratio is 6.0. The blower room houses 5 Roots blowers (4 in operation, 1 standby), each with a flow rate of 105 m³/min and a unit power of 185 kW.
The AAO process has two biological reaction tanks, each with a treatment capacity of 50,000 m³/d. For each tank, the effective volumes of the anaerobic zone, anoxic zone, and aerobic zone are 3,168 m³, 13,475 m³, and 19,866 m³, respectively. The effective water depth is 6.0 m, the external sludge recirculation ratio is 100%, the internal recirculation ratio is 300%, and the design HRT is 17.5 hours (anaerobic: 1.5 h, anoxic: 6.5 h, aerobic: 9.5 h). The sludge age in the aerobic zone is 8.9 days, and the design air-to-water ratio is 6.2. The anaerobic zone consists of 2 compartments, each with dimensions of 6 m × 44 m. The anoxic zone consists of 8 compartments, each 7 m × 44 m. To keep the sludge in suspension and ensure sufficient mixing with the influent, submersible mixers are installed in the anaerobic and anoxic zones: 4 units per tank in the anaerobic zone (P=6 kW) and 12 units per tank in the anoxic zone (P=7 kW). The aerobic section has 6 compartments, each 11 m × 44 m, plus 1 effluent compartment of the same size. There are 5 blowers in total (4 in operation, 1 standby): 3 are Roots blowers, each with a flow rate of 61.5 m³/min, a pressure of 68.6 kPa, and a unit power of 132 kW; 2 are centrifugal blowers with variable frequency drives, each with a flow rate of 185 m³/min and a power of 185 kW. The oxygen supply equipment in the tank consists of 1,300 fine bubble membrane diffuser tubes, each 1,000 mm long.
1.2 Off-Gas Analysis Process
The off-gas test method is based on the US "Clean Water Oxygen Transfer Test Standard." It calculates oxygen utilization by the activated sludge by measuring the remaining oxygen content in the off-gas using an off-gas analyzer.
1.3 Determination of Specific Ammonia Utilization Rate (SAUR)
Add 1.0 L of activated sludge from the aerobic tank to a beaker and aerate with an air pump for 30 minutes, controlling the Dissolved Oxygen (DO) concentration between 5-6 mg/L. Add 5 mL of NH₄Cl solution and 5 mL of NaHCO₃ solution to the sample. At regular intervals, extract 20 mL of mixed liquor from the beaker using a syringe, filter it, and measure the Ammonia Nitrogen (NH₄⁺-N) concentration in the filtrate. Perform linear fitting between the NH₄⁺-N concentration and reaction time; the slope is the nitrification rate. Additionally, take 100 mL of activated sludge for MLSS measurement. Dividing the nitrification rate by the MLSS gives the Specific Ammonia Utilization Rate (SAUR) in mg/(g·h).
1.4 Determination of Microbial Population Abundance
Sludge samples were taken from the aerobic tanks of the MBBR and AAO processes. Each group had three parallel samples, stored at -18°C to ensure sample integrity. They were then sent to a professional biotechnology company for analysis using the Illumina MiSeq high-throughput sequencing platform. Following the method reported by ZHOU et al., genomic DNA was extracted; the obtained DNA was ligated with specific primers to synthesize primer adapters; target fragments were amplified via Polymerase Chain Reaction (PCR); amplification products were purified, and Miseq libraries were constructed; high-throughput sequencing of the constructed libraries was performed using the Illumina MiSeq platform.
2 Results and Analysis
2.1 Analysis of Process Operation Performance
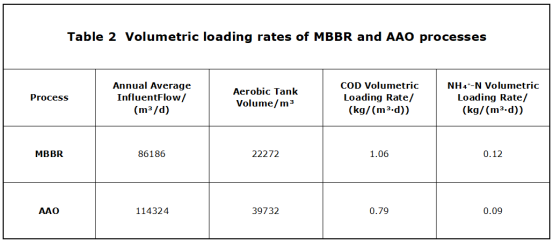
The annual removal efficiencies of organic matter and nitrogenous pollutants in the wastewater treatment plant are shown in Figure 2. The MBBR and AAO processes share the same influent quality. The high proportion of industrial wastewater results in high influent pollutant loads. The concentrations of COD, Total Nitrogen (TN), and NH₄⁺-N in the influent fluctuate significantly, increasing the difficulty of maintaining stable effluent compliance. However, both processes can effectively handle the high influent loads and severe seasonal water quality fluctuations, producing stable effluent quality that exceeds the Grade A standard. The actual annual average daily influent flows for the MBBR and AAO processes were 86,186 m³/d and 114,324 m³/d, respectively. The average removal rates for COD, NH₄⁺-N, and TN in the MBBR process were 92.6%, 98.2%, and 78.6%; for the AAO process, they were 92.9%, 98.5%, and 79.2%.
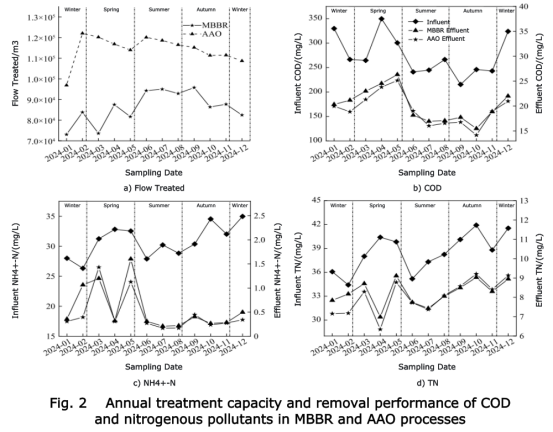
The annual average influent COD concentration for both processes was 274.3 mg/L, and the NH₄⁺-N concentration was 30.8 mg/L. The volumetric loading rates for the MBBR and AAO processes were calculated based on the annual average actual influent flow and aerobic tank volume, as shown in Table 2. The COD and NH₄⁺-N volumetric loading rates for the MBBR process were 26.7% and 28.0% higher than those of the AAO process, achieving more efficient pollutant removal in a smaller tank volume. This is because the addition of suspended carriers increases the biomass in the reactor and optimizes the structure of the microbial community, significantly enhancing the degradation efficiency of microorganisms within the reactor.
2.2 Nitrification Rate Analysis
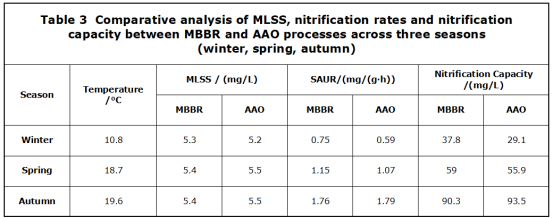
The MLSS, SAUR, and nitrification capacity of the activated sludge containing suspended carriers from the MBBR process and the activated sludge from the AAO process were measured in autumn, winter, and spring, as shown in Table 3. The differences in SAUR between the MBBR and AAO processes in spring and autumn were not significant. However, as temperatures decreased, the enhancement effect of suspended carriers on the nitrification capacity of the sludge mixed liquor gradually became apparent. Under low-temperature conditions in winter, the growth and activity rates of nitrifying and denitrifying bacteria significantly decrease, leading to a reduction in SAUR for both processes. However, under these conditions, the MBBR process showed significant improvements in both SAUR and nitrification capacity compared to the AAO process. In winter, the SAUR for the MBBR and AAO processes were 0.75 mg/(g·h) and 0.59 mg/(g·h), respectively, with corresponding nitrification capacities of 37.8 mg/L and 29.1 mg/L. Specifically, the SAUR of the MBBR process was 27.1% higher than that of the AAO process, and the nitrification capacity was 29.9% higher. Liu Qiang et al. demonstrated that the MBBR process, by strengthening the synergistic effect between biofilm and activated sludge, can maintain a 19.6% to 27.4% higher nitrification capacity than the AAO process even under low-temperature conditions below 11°C, significantly enhancing the system's resistance to low-temperature shocks. The MBBR process effectively addresses the attenuation of nitrification efficiency caused by low temperatures by constructing a biofilm micro-ecological environment.
2.3 Microbial Population Analysis
Figure 3 shows the distribution of sludge from the MBBR and AAO aerobic tanks at the phylum level. Nitrifying functional bacteria mainly include Ammonia-Oxidizing Bacteria (AOB) and Nitrite-Oxidizing Bacteria (NOB), whose core groups mostly belong to the Proteobacteria and Nitrospirae phyla. Proteobacteria had the highest relative abundance in both the MBBR and AAO processes, at 30.9% and 25.2%, respectively. As typical nitrifying functional bacteria, Proteobacteria are common microbial groups involved in nitrogen transformation in wastewater treatment processes, encompassing all AOB and NOB among nitrifying bacteria. The proportion of this phylum can, to some extent, reflect the nitrification activity in the aerobic tank of a wastewater treatment plant. Bacteroidetes was the second most abundant phylum in both the MBBR and AAO processes, with relative abundances of 28.5% and 23.2%, respectively. Bacteria in the Bacteroidetes phylum play important roles in organic matter degradation and nitrogen transformation. By improving the stability of the microbial community and promoting organic matter degradation, they can indirectly enhance the efficiency of the nitrification process. Han Wenjie et al. conducted a systematic study on the impact of low-temperature environments on the MBBR process. By comparing winter operational data from five wastewater treatment plants using this process in the Yangtze River Delta region, they found that the addition of suspended carriers significantly increased the biomass of nitrifying bacterial communities within the system. The enrichment of nitrifying bacteria in the suspended carrier biofilm accounted for 86.1% to 95.4% of the total system biomass, confirming the directional enrichment effect of suspended carriers on nitrifying functional bacteria groups.
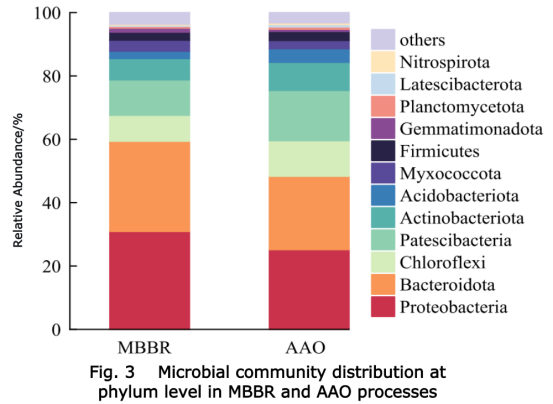
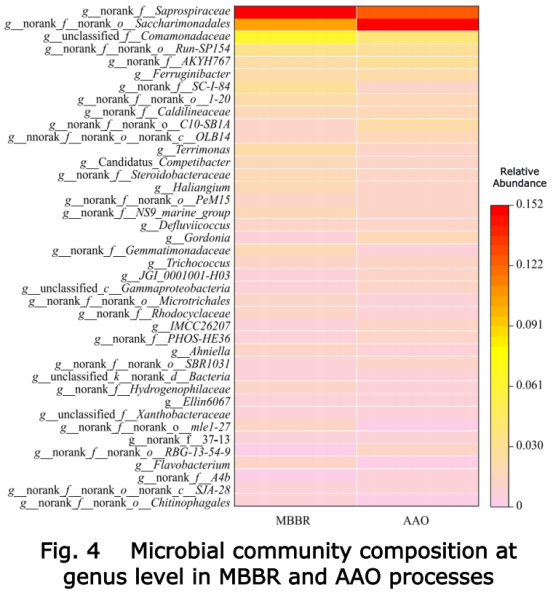
Figure 4 shows the distribution of sludge from the MBBR and AAO process aerobic tanks at the genus level. Among them, g__norank_f__NS9_marine_group is an autotrophic nitrifying bacterium. Its relative abundances in the MBBR and AAO process activated sludge were 1.6% and 1.2%, respectively. This genus plays an important role in promoting nitrification. g__norank_f__norank_o__Chitinophagales has heterotrophic nitrification characteristics, with relative abundances of 1.0% and 0.3% in the two processes, respectively. Simultaneously, g__Ellin606 is also a known autotrophic nitrifying bacterium, with relative abundances of 0.92% and 0.66% in the two processes, respectively. At the genus level of microbial population distribution, it can also be indicated that the MBBR process has stronger nitrification treatment capability compared to the AAO process.
2.4 Energy Consumption Statistical Analysis
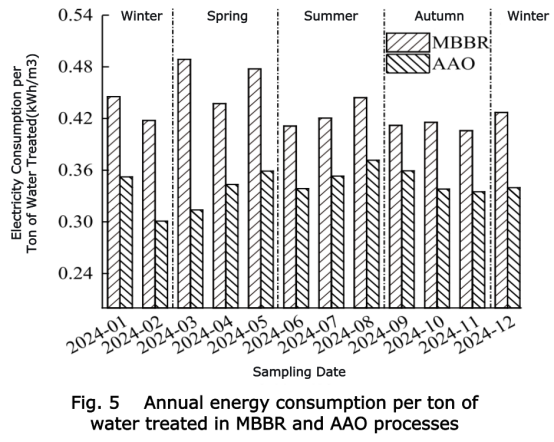
- Annual Electricity Consumption per Ton of Water Treated. The monthly electricity consumption per ton of water treated for the MBBR and AAO processes is shown in Figure 5. The electricity consumption for the MBBR process was (0.43 ± 0.03) kWh/m³, higher than the national average of 0.33 kWh/m³ for wastewater treatment plants. The AAO process's (0.34 ± 0.02) kWh/m³ was on par with the national average. Compared to the electricity consumption per ton of water in developed countries' wastewater treatment plants (0.20-0.32 kWh/m³), both processes have room for energy saving and consumption reduction. The annual electricity consumption per ton of water for both processes showed obvious seasonal variation. The consumption was higher in spring and summer and lower in autumn and winter, following the pattern of treated water volume for both processes. The monthly electricity consumption per ton of water for the MBBR process was consistently higher than that of the AAO process throughout the year, averaging 26.5% higher annually.
- Analysis of Energy Consumption Distribution by Unit. The plant's equipment was divided into the following units for statistical analysis: Power Lift Unit, Pretreatment Unit, Biological Treatment Unit, Tertiary Treatment Unit, Sludge Treatment Unit, and Deodorization Unit. Statistics were collected on equipment rated power, actual operating units, and effective operating time, corrected with actual electricity meter data. All collected data were annual averages, and the results are shown in Figure 6. The energy consumption of the Biological Treatment Unit is mainly concentrated on blowers, submersible mixers, and internal/external recirculation pumps. It is the unit with the highest energy consumption share, accounting for 57.8% and 52.1% of the total energy consumption of the MBBR and AAO processes, respectively, similar to other wastewater treatment plants in China (45%-55%).
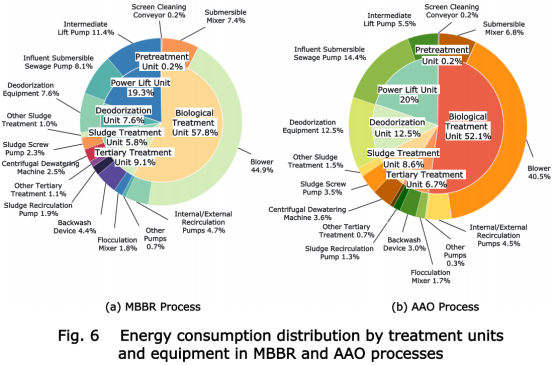
The specific energy consumption of the Biological Treatment Unit for the MBBR process was 0.25 kWh/m³, which is 38.9% higher than that of the AAO process (0.18 kWh/m³). Blowers accounted for 44.9% and 40.6% of the total energy consumption of the two processes, respectively, making them the equipment with the highest energy consumption share. Because the MBBR process requires additional air volume to maintain the fluidization state of the suspended carriers, its blower specific energy consumption was 0.19 kWh/m³, higher than the AAO process's 0.14 kWh/m³.
The Power Lift Unit mainly includes influent submersible sewage pumps and lift pumps, accounting for 19.3% and 20.0% of the total energy consumption of the MBBR and AAO processes, respectively, making it the second-largest unit in terms of energy consumption share. The Deodorization Unit accounted for 7.6% and 12.5% of the total energy consumption of the MBBR and AAO processes, respectively. Although often overlooked in energy consumption statistics, the Deodorization Unit has a high energy consumption share, second only to the Power Lift Unit. The Tertiary Treatment Unit mainly includes mixing/flocculation agitators and backwash devices, accounting for 9.1% and 6.7% of the total energy consumption of the MBBR and AAO processes, respectively. The Sludge Treatment Unit mainly includes centrifugal dewatering machines and sludge screw pumps, accounting for 5.8% and 8.6% of the total energy consumption of the MBBR and AAO processes, respectively. The Pretreatment Unit mainly includes coarse and fine screen cleaners and conveyors, with a very small energy consumption share.
2.5 Comprehensive Process Energy Efficiency Comparison
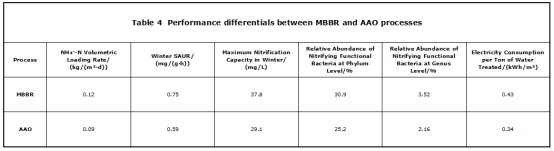
Integrating the above analysis results of process operation performance and energy consumption, the performance differences between the MBBR and AAO processes were comprehensively assessed, as shown in Table 4. The MBBR and AAO processes showed significant differences in winter SAUR, relative abundance of nitrifying functional bacteria, and electricity consumption per ton of water. The characteristics of the MBBR process increase the biomass in the biological tank and directionally enrich nitrifying functional bacteria, significantly enhancing the system's nitrification capacity and resistance to low-temperature shocks. The winter SAUR of the MBBR process was 27.1% higher than that of the AAO process, the maximum winter nitrification capacity was 29.9% higher, the relative abundance of nitrifying functional bacteria at the phylum level was 22.6% higher, and the relative abundance of nitrifying functional bacteria at the genus level was 63.0% higher. Although the MBBR process demonstrated superior performance in SAUR and abundance of nitrifying functional bacteria, its energy consumption increased significantly. Aeration in the MBBR process must fulfill a dual task: meeting the oxygen demand of microorganisms while maintaining the fluidization state of suspended carriers in the biological reaction tank, which directly leads to increased energy consumption. The electricity consumption per ton of water for the MBBR process was 26.5% higher than that of the AAO process.
2.6 Energy-Saving Optimization Measures for the MBBR Process Aeration System
Operational data indicate that the actual average air-to-water ratio for the MBBR process reached 9.13, while it was 6.42 for the AAO process. The MBBR process's air-to-water ratio was 42.2% higher than that of the AAO process. The Off-Gas Analysis method was used for on-site measurement of the Oxygen Transfer Efficiency (OTE) of both processes. The results showed that the OTE value for the MBBR process was 11.9%, significantly lower than the AAO process's OTE value of 25.8%, only 46.1% of the latter.
The wastewater treatment plant's MBBR process uses two air supply methods: perforated pipe aeration and fine bubble aeration. However, both are supplied by the same main air supply pipe. Since the air resistance of perforated pipes is lower than that of fine bubble diffusers, the vast majority of the air volume escapes from the perforated pipes, greatly reducing the oxygen transfer performance of the aeration system. The perforated aeration system ensures the fluidization state of the suspended carriers. The kinetic energy of bubbles from the perforated aeration system can effectively prevent the accumulation of suspended carriers (suspended carrier movement velocity > 0.3 m/s), but the generated bubbles are larger (3-5 mm in diameter), leading to reduced gas-liquid contact area, shortened gas-liquid contact time, and OTE lower than that of fine bubble aeration (bubble diameter 0.2-2 mm). Research by Collivignarelli et al. indicates that although the coarse bubble aeration system using perforated pipes in the MBBR process has certain advantages in reducing fouling, its OTE is lower, which involves higher operational costs. McQuarrie et al. showed that fine bubble diffusers have higher OTE than coarse bubble diffusers, while freely moving suspended carriers can affect the OTE value of the MBBR process. Therefore, it is recommended to supply the perforated pipe and fine bubble aeration equipment with separate, dedicated blowers and air pipes.
According to the "Technical Specification for Municipal Wastewater Treatment by Moving Bed Biofilm Reactor" (T/CUWA-2021), to ensure good fluidization of suspended carriers and full mixing with activated sludge, the aeration intensity should not be less than 3 m³/(m²·h). Therefore, the air supply rate qm for the perforated aeration system is calculated according to Equation (1).
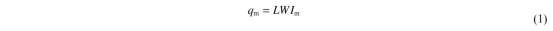
In the equation: qm is the air supply rate, m³/h; L is the length of the suspended carrier addition zone, m, which is 78.6; W is the width of the suspended carrier addition zone, m, which is 44.0; Im is the minimum aeration intensity to maintain carrier fluidization, m³/(m²·h), which is 3.
According to Equation (1), the calculated air supply rate qm for the perforated aeration system is 10,368 m³/h. While maintaining the fluidization state of the suspended carriers, the perforated aeration system also provides part of the oxygen required for pollutant removal. The remaining oxygen demand is provided by the fine bubble aeration system. The air supply rate qf for the fine bubble aeration system is calculated according to Equation (2).
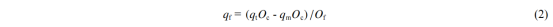
In the equation: qf is the air supply rate of the fine bubble aeration system, m³/h; qt is the annual average daily air volume, m³/h, which is 33,728; Oc is the Oxygen Transfer Efficiency of the perforated pipe aerator, %, which is 11.9; Of is the Oxygen Transfer Efficiency of the fine bubble aerator, %, which is 25.8.
The calculation shows that the air supply rate qf for the fine bubble aeration system is 10,775 m³/h. Therefore, supplying the perforated and fine bubble aeration systems separately would require only 21,143 m³/h of daily average air volume, saving 37.3% of the air volume. The blower specific energy consumption for the MBBR process could be reduced to 0.12 kWh/m³, and the overall specific energy consumption of the MBBR process could be reduced to 0.36 kWh/m³.
3 Conclusion
- Adding suspended carriers in the MBBR process can improve the loading capacity and SAUR of the biological reaction tank. The COD volumetric loading rate and NH₄⁺-N volumetric loading rate of the MBBR process were 26.7% and 28.0% higher than those of the AAO process, respectively. In winter low temperatures, the SAUR of the MBBR process increased by 27.1% compared to the AAO process, and the nitrification capacity increased by 29.9%.
- The MBBR process enriched more nitrifying functional bacteria compared to the AAO process. The relative abundance of nitrifying functional bacteria at the phylum level in the MBBR process was 22.6% higher than in the AAO process, and at the genus level, it was 63.0% higher. This indicates, from the perspective of microbial population distribution, that the MBBR process enhances the nitrification function in the aerobic tank.
- The electricity consumption per ton of water for the MBBR process was 26.5% higher than that of the AAO process, and the specific electricity consumption of the Biological Treatment Unit in the MBBR process was 47.1% higher than that of the AAO process. Blower energy consumption accounted for up to 44.9% of the total energy consumption in the MBBR process and 40.6% in the AAO process. The blower energy saving potential in the Biological Treatment Unit of the MBBR process is relatively large.
- The additional perforated pipe aeration used in the MBBR process lowers the OTE of aeration, requires more energy consumption, and has significant energy-saving potential. Supplying the perforated pipe and fine bubble aeration equipment with separate air sources could reduce the specific energy consumption of the MBBR process to 0.36 kWh/m³.